Engineering article
What happens to heavy Twill fabric when sheared?
An engineering look at a heavy 600gsm 12K fabric: how shear changes internal tuft geometry and why test laying is more important than external smoothness.
Heavy fabric quickly gains reinforcement, but requires space
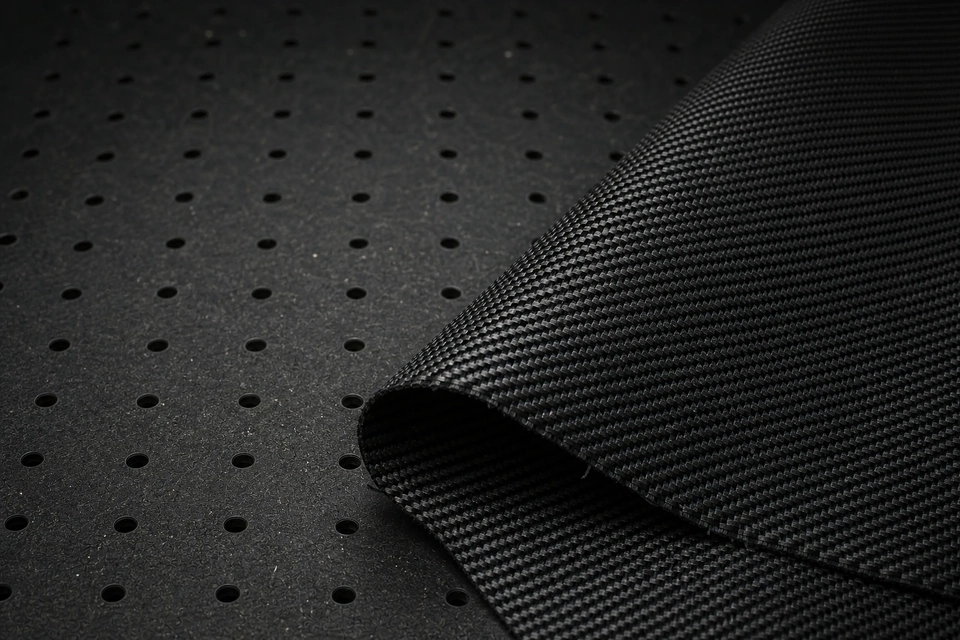
The 600 g/m² fabric allows you to add a significant amount of fiber in one layer. This reduces the number of operations in a thick bag, but large 12K bundles take up more volume and do not follow tight radii as readily as lighter fabrics. On a flat panel this can be an advantage, but on a deep form it can be a source of local compaction. Therefore, “gain thickness faster” and “easier to mold the part” are different goals: they cannot be combined with one choice of density.
Tomography reveals what is not visible on the surface
In a study of twill fabric, shear deformation was studied using microtomography. As the angle between the directions changed, not only the contours of the cell changed, but also the shape of the bundles, as well as the local orientation of the fibers within them. This is an important observation for practice: a smooth outer side does not yet prove the uniformity of the internal structure. The yarns can flatten, rotate and crowd each other, and such changes then affect the penetration and repeatability of the laminate.
Where does technological risk occur most often?
The most demanding areas are those where the curvature changes in two directions at once, as well as internal corners, narrow bridges and transitions to the edge. If the fabric is fixed at the edges too early, the excess length may accumulate in one place. If the fixation is weak, the pattern and direction of the reinforcement shifts. For heavy Twill fabric, it is important to think in advance about the laying order, the position of cuts or overlaps, and how to hold the blank before vacuuming. These decisions are checked on the form, and not on a photograph of the roll.
What to send to calculate the factory position
For CC-CF-032, you need to specify the required roll width, total required length or lot weight, forming process and part purpose. If the material is selected for a specific equipment, attach a model or several views with marked radii. It is useful to indicate the permissibility of joints and the direction of the visible pattern. Since the position belongs to the factory programme, the price is formed on quotation after confirmation of the volume and lead time. It makes sense to approve a trial cut or process trial before the main batch if the geometry of the product is not flat.